
A wear layer is a clear polyvinyl chloride (PVC) film that shields resilient flooring from everyday scratches, scuffs and surface wear. It is typically manufactured separately and then laminated onto a printed vinyl sheet. The sheet is then embossed and finished with a thin protective coating that is cured with ultraviolet (UV) light before the plank is cut to size.
The wear layer and the coating on top serve separate functions: the wear layer is the component whose thickness is marketed as ‘12 mil’ or ‘20 mil,’ while the coating is a much thinner surface finish applied above it.
The whole sequence typically happens on a single production line, in roughly this order: print the design, laminate on the clear PVC wear layer, emboss the texture, apply and cure the protective coating, then cool and cut. The exact line setup varies by manufacturer.
Understanding how a wear layer is manufactured explains why the clear layer looks the way it does, why the thickness printed on the box is a real physical measurement, and why its surface texture lines up so precisely with the printed pattern underneath.
Preparing for the Wear Layer
Before the clear layer is applied, the plank already has a core and a printed design layer. A base sheet is formed through calendering — a process that runs softened vinyl compound through a series of heated rollers to set its thickness and smooth its surface — or through extrusion for composite cores. A printed film showing the wood or stone pattern is then bonded to that base under heat and pressure.
This holds true across the different core types used in resilient flooring: a flexible luxury vinyl tile (LVT) core, a rigid stone plastic composite (SPC) core or a cushioned wood plastic composite (WPC) core with a waterproof base. Although the core construction varies by product category, the wear layer applied over the printed design follows a broadly similar process in each.
The clear PVC wear layer is laminated onto the printed sheet under heat and pressure, then typically finished with a separate UV-cured coating rather than brushed on by hand.
How the Wear Layer is Applied
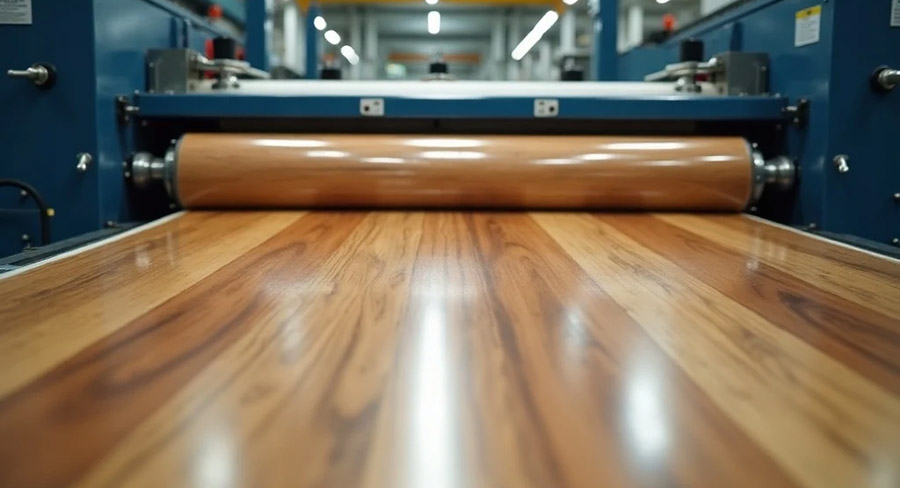
The clear PVC wear layer is a separate, already-manufactured sheet of clear PVC film. That film is fed onto the printed layer and bonded to it using rollers under heat and pressure — the same type of process that bonded the printed film to the core in the previous step. The result is a single fused sheet: core, print and clear wear layer pressed together as one.
This is the layer that carries the thickness rating printed on the box, usually given in mils (a mil meaning one-thousand of an inch). A 20-mil wear layer is roughly 0.5 millimetres (mm) of clear PVC; a 12-mil wear layer is about 0.3 mm. A higher rating means a thicker PVC film was used at this lamination stage, not a heavier application of anything applied later. That later step — a thin protective coating — is a different layer entirely.
The Role of a Protective Coating
Most LVT, SPC and WPC products add a thin urethane or acrylic coating over the wear layer, cured with UV light. This hardens the surface finish almost instantly and consistently, without the slower dry time of air curing. The coating is substantially thinner than the wear layer underneath it.
The coating is applied as a liquid resin rolled onto the wear layer in a thin, even film. Because it starts as a liquid, it can be spread in a finely controlled thickness and settle into fine surface detail before it hardens. This step typically comes after the wear layer has been laminated and embossed, so the UV-cured finish protects the textured surface rather than sitting underneath it. The exact order, however, can vary by manufacturer and production line.
Curing works by exposing the freshly applied coating to UV light on the production line. That exposure triggers a chemical reaction in the coating called polymerization, which rapidly links its molecules into a solid, stable structure. The plank comes out the other end of that stage of the line with a fully set surface in a matter of seconds.
This step matters for consistency as much as speed. Because every square metre of the sheet passes under the same UV exposure at the same line speed, the resulting surface hardness and clarity are consistent across an entire production run. Manufacturing consistency is one of several factors that influence how a floor holds up over time.
The embossing step is also important to how the finished floor looks and feels. Rollers press texture into the wear layer itself, following the printed pattern beneath it.
Matching EIR Texture to the Print
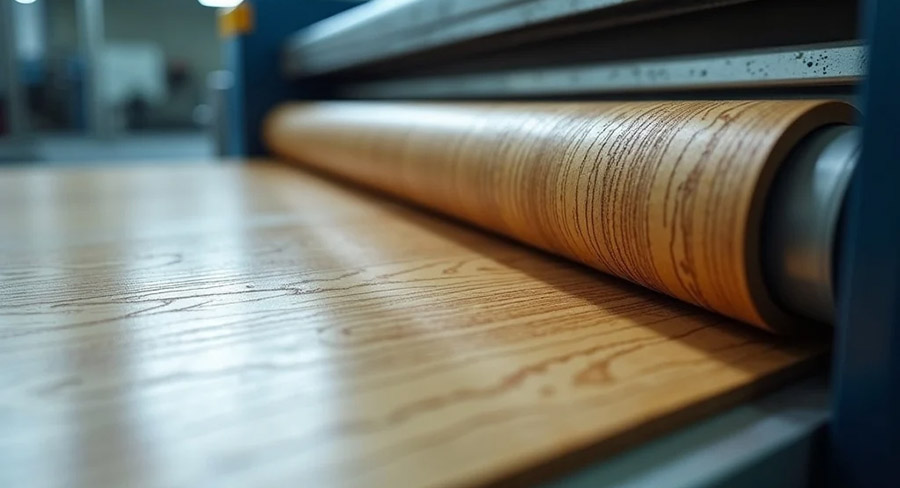
Embossed-in-register (EIR) texture is created by pressing a textured roller or plate into the wear layer at the precise position on the plank where the corresponding detail appears in the printed layer beneath it. That alignment is what ‘in register’ means: the physical texture and printed image are registered, or synchronized, with each other.
Mechanically, this requires the embossing stage of the line to track the position of the printed pattern as it moves, usually through a registration mark or sensor built into the printed film. This allows the embossing plate to press its grooves and ridges into the corresponding spot as each plank passes through, rather than setting the position just once at the start of a run. The exact sensors and hardware used to maintain that registration can vary by equipment and production line. Where the printed image shows a knot or a deep grain line, the embossed texture underfoot has a corresponding dip or ridge in that same location. By contrast, standard, non-registered embossing generally presses a texture across the whole sheet without tracking the print. The result can feel slightly mismatched to the image, with texture in one place and flat print in another.
Quality Checks on the Production Line
Manufacturers typically monitor wear layer thickness and surface quality during production, using quality control procedures that may include thickness measurements, visual inspections, gloss measurements, adhesion testing and abrasion testing.
Thickness checks confirm that the clear PVC wear layer was laminated at an even thickness across the plank, since the mil rating advertised on the box only means something if the layer is genuinely that thick throughout, not just in the middle. Gloss and adhesion checks focus on the UV-cured coating applied above the wear layer, confirming that the finish matches the intended sheen (matte, satin or higher) and has bonded properly to the surface beneath it. Visual inspection, whether performed by trained line staff, automated optical scanning or a combination of both, checks for surface clarity, consistent embossing registration and the absence of visible defects before the sheet moves on to cutting. The exact instruments and inspection intervals vary by manufacturer and production line.
Rob Banks is CEO of Caledon Floors, a Canadian flooring brand based in Vancouver that focuses on premium hard surface flooring sold through independent flooring dealers rather than directly to consumers. The company’s product line includes Goliath, Artimis, Monolith and Origins. Rob can be reached at [email protected].